skip to Main Content

Top Machining Parts Suppliers for Global Buyers

Global manufacturers are seeking faster, more reliable, and more traceable sourcing options. Machining Parts remain essential for aerospace, automotive, medical equipment, robotics, and industrial machinery. Grand View Research identifies continued growth in the global CNC machine market, driven by automation, precision requirements, and shorter production cycles. These trends are changing how buyers evaluate suppliers.

Price alone is no longer enough. A capable supplier should demonstrate stable tolerances, documented inspection procedures, responsive engineering support, and dependable export experience. ISO 9001 certification can indicate a structured quality system, although certification does not guarantee perfect workmanship. Buyers should still review sample reports, material certificates, process controls, and first-article inspection records.

The 2024 Deloitte Global Manufacturing Industry Outlook also highlights digital transformation, supply-chain resilience, and workforce capability as major manufacturing priorities. For international buyers, these priorities appear in practical details: a supplier answering technical questions clearly, updating production status, and protecting drawings through controlled communication. Small delays can disrupt an entire assembly line.

This guide examines leading Machining Parts suppliers for global buyers. It considers machining capacity, material knowledge, surface finishing, quality assurance, minimum order quantities, lead times, and communication standards. The comparison is useful, but no supplier is ideal for every application. A low-volume prototype requires different strengths than a certified aerospace production program.

The market is not perfectly predictable. Buyer requirements also change. Careful verification remains essential.
Top Machining Parts Suppliers for Global Buyers

Machining Parts Suppliers: Scope, Processes, and Global Market Roles

Machining parts suppliers serve as technical partners for global buyers, not merely production vendors. Their scope may include prototypes, low-volume batches, and continuous production. Common processes include CNC milling, turning, grinding, drilling, and surface finishing. Experienced suppliers interpret drawings, identify difficult tolerances, and recommend practical materials. A 0.01 mm tolerance can change machining time, inspection needs, and total cost. Good suppliers explain these effects before production begins.

Tips: Request sample inspection reports, material certificates, and process details. Confirm tolerance capability with measured evidence, not promises. Ask how suppliers control tool wear, because small changes can affect fit. Keep communication precise. A clear drawing prevents expensive assumptions.

In the global market, suppliers connect engineering teams, factories, and purchasing departments across borders. They may support packaging, production scheduling, customs documents, and traceability records. Reliable partners use calibrated equipment and maintain inspection checkpoints during production. Coordinate time zones carefully. A missed clarification can delay an entire shipment. No supplier is perfect, and a polished website proves little. Buyers should review trial parts, communication habits, corrective actions, and delivery history. I have found that the strongest relationships grow from transparent problem-solving, even when the first batch needs adjustment. Cost matters, but repeatable quality usually protects the larger investment.

Machining Parts Suppliers: Scope, Processes, and Global Market Roles

The chart compares typical achievable dimensional tolerances for major machining processes. Actual results depend on machine condition, material, geometry, tooling, inspection methods, and supplier quality systems. Suppliers commonly combine milling, turning, grinding, and EDM to support prototypes, production parts, and high-precision components.

Quality Benchmarks: ISO 9001, ±0.01 mm Tolerances, and Inspection Methods

Global buyers often compare machining suppliers by price, but quality benchmarks reveal more. ISO 9001 certification shows that a supplier controls documented processes, corrective actions, and production records. It does not guarantee every part is perfect. Buyers should review audit status, calibration records, and recent inspection reports.

A ±0.01 mm tolerance requires more than a capable machine. Material stability, tool wear, temperature, and operator technique can all affect results. Experienced suppliers inspect critical dimensions with calibrated micrometers, gauges, and coordinate measuring machines. First-article inspection confirms the drawing before volume production begins. Batch reports should identify measurements, equipment, and inspection dates. Small details matter.

Tips: Ask whether the quoted tolerance applies to every feature or only selected dimensions. Request a sample report before placing an order. Confirm how rejected parts are isolated and corrected. A clear inspection plan prevents expensive surprises.

In practice, even well-managed production can show variation. We once found a nearly acceptable bore size after repeated checks; the measurement method, not the part, caused confusion. That experience reinforced a simple lesson: inspection procedures need review, not blind trust. Suppliers should explain their measurement uncertainty and define acceptance criteria in writing. Reliable communication, traceable records, and honest discussion of limits help global buyers choose machining partners with confidence.

Top Machining Parts Suppliers for Global Buyers - Quality Benchmarks: ISO 9001, ±0.01 mm Tolerances, and Inspection Methods

The following table presents practical industry benchmarks for evaluating machining-part suppliers. Values are typical reference ranges rather than claims about any specific company, facility, or brand.

Evaluation Dimension Recommended Benchmark Typical Evidence or Deliverable Common Verification Method Buyer Consideration
Quality management system ISO 9001 certified Current certificate showing the legal entity, site address, scope, and certificate validity period Verify the certificate number and issuing certification body through an accredited certification directory Confirm that the certificate scope covers machining, fabrication, inspection, or the services being purchased
Standard CNC milling tolerance ±0.05 mm for suitable features; tighter values available by drawing agreement Dimensional inspection report linked to the part drawing and revision level Calibrated vernier calipers, micrometers, height gauges, or coordinate measuring machines Do not apply ±0.01 mm to every feature without considering material, geometry, size, and process capability
Precision tolerance capability ±0.01 mm on selected, well-controlled features Capability study, first-article report, and measurement results for critical dimensions Coordinate measuring machine, air gauge, bore gauge, or calibrated micrometer, depending on geometry Request confirmation of achievable tolerance before quotation; tolerance may require additional operations or inspection cost
CNC turning tolerance ±0.02–0.05 mm for common turned dimensions; tighter limits by agreement Inspection report covering diameters, lengths, threads, concentricity, and surface finish Outside micrometer, bore gauge, thread gauges, optical comparator, or CMM Check whether tolerances apply to diameters, shaft lengths, threads, or geometric relationships
Geometric tolerancing GD&T applied to critical features, including position, flatness, perpendicularity, and concentricity where needed Drawing review records and inspection results reported against the specified datum structure CMM, surface plate with height gauge, dial indicator, or optical measurement system Use a clear datum scheme to prevent different interpretations between buyer and supplier
Surface roughness Ra 1.6–3.2 µm for many machined surfaces; lower Ra values require defined finishing processes Surface-finish results identified by feature and measured area Contact or non-contact surface roughness tester with a valid calibration status Specify the measurement direction, cutoff length, sampling location, and whether the value is before or after coating
Dimensional inspection coverage 100% inspection for critical characteristics; sampling for stable, non-critical features Inspection plan defining characteristic classification, sample size, equipment, and acceptance criteria Review inspection records and compare them with the control plan and technical drawing Critical-to-function dimensions should be identified before production begins
First Article Inspection Recommended for new parts, major revisions, or process changes FAI report containing ballooned drawing, material certificates, process records, and measured results Document review against the approved drawing revision and purchase-order requirements FAI reduces the risk of repeated production of an incorrect part
Material traceability Required for regulated or safety-critical parts Mill test certificate, heat or lot number, material grade, and traceability records Cross-check material certificates with part markings, purchase records, and supplier documentation Define acceptable material standards, substitutions, and certificate language in the purchase order
Coating and surface-treatment control Process specification, thickness target, appearance criteria, and corrosion-performance requirement when applicable Plating, anodizing, passivation, heat-treatment, or coating certificate Coating thickness gauge, hardness tester, visual inspection, or laboratory test report Confirm whether coating dimensions are included in the final tolerance requirements
Calibration system All measuring equipment traceable to recognized standards Calibration certificates, equipment identification numbers, and calibration due dates Audit equipment records and verify that instruments used for acceptance were in calibration Measurement uncertainty should be appropriate for the tolerance being evaluated
Nonconformance management Documented segregation, root-cause analysis, corrective action, and disposition process Nonconformance report, corrective-action report, rework record, or concession approval Review closed cases and confirm that unauthorized deviations are not shipped Require written approval for use-as-is, repair, rework, or deviation from the drawing
Production capacity transparency Capacity stated by machine type, working envelope, material, and monthly or weekly availability Capacity plan, production schedule, and documented subcontracting controls where relevant Technical review, sample order, or supplier audit Capacity should be evaluated together with inspection resources and process stability
Prototype lead time Approximately 5–15 working days for straightforward CNC prototypes after drawing approval Quotation with assumptions for material, finishing, inspection, packaging, and shipping Compare quoted lead time with actual milestone dates during a pilot order Complex materials, special coatings, tooling, and third-party testing can extend the schedule
Production lead time Approximately 2–6 weeks for many repeat orders, subject to volume and process complexity Order confirmation, production schedule, inspection-release date, and shipping plan Track on-time delivery over multiple purchase orders rather than relying on one shipment Separate manufacturing lead time from international transit and customs clearance
Pre-shipment documentation Recommended for international orders and controlled parts Commercial invoice, packing list, certificate of conformity, inspection report, and material certificates where required Document checklist review before shipment release Agree in advance on file format, language, retention period, and approval responsibility

Supplier Capabilities: CNC, 5-Axis, Turning, Materials, and Annual Capacity

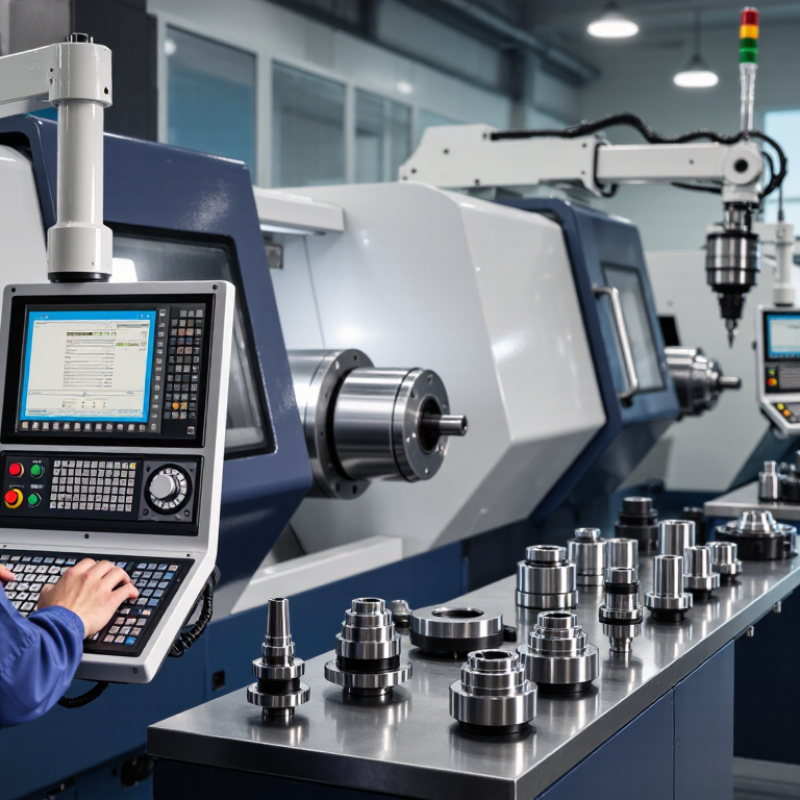
For global buyers, machining capability should be measured beyond equipment lists. A reliable supplier should explain its CNC process, work envelope, tolerances, and inspection methods. Ask whether operators verify first articles with calibrated gauges or coordinate measuring machines. Small details matter. A clean inspection report should identify material grade, dimensions, surface finish, and batch number.

Five-axis machining can reduce setups and improve access to complex surfaces. It suits impellers, medical housings, aerospace brackets, and other parts with angled features. However, five-axis equipment does not guarantee accuracy. Programming experience, fixture design, and machine calibration remain decisive. Turning suppliers should show their ability to control concentricity, threads, grooves, and thin-wall deformation. Sample drawings reveal more than polished photographs.

Material knowledge also separates capable suppliers from general workshops. Aluminum, stainless steel, titanium, brass, engineering plastics, and tool steel require different cutting speeds and inspection controls. Buyers should request traceable material certificates and confirm heat-treatment options when needed. Annual capacity must be discussed carefully. A quoted volume may describe theoretical machine hours, not dependable output. Ask for current utilization, backup equipment, average batch size, and realistic monthly capacity. Capacity is not unlimited.

An experienced supplier will also explain weak points instead of promising everything. Some estimates may need revision after reviewing tolerances or surface requirements. That honesty is useful. It exposes risk before production begins and supports a more reliable sourcing decision.

Global Comparison: Lead Times, MOQ, Certifications, and Unit-Cost Factors

Top Machining Parts Suppliers for Global Buyers

Lead time, MOQ, certifications, and unit cost often matter more than the lowest quotation. A 2023 global logistics report recorded continued freight-rate volatility, making a 10-day machining lead time less useful if transport adds three weeks. Request a production schedule with material arrival, first-article inspection, and dispatch dates.

For prototypes, an MOQ of one to ten pieces is practical. For repeat orders, suppliers may reduce unit prices above 100 or 500 pieces. Yet, a large MOQ can trap cash in slow-moving inventory.

Certification needs careful checking. The ISO Survey 2022 reported more than 1.26 million valid ISO 9001 certificates worldwide. However, certification alone does not prove process capability. Ask for the certificate scope, expiry date, calibration records, and inspection reports. For aerospace, medical, or automotive work, additional standards may apply.

Unit cost should include tooling, programming, surface treatment, packaging, duties, and freight. A cheaper quote can become expensive after these additions. This is where buyers sometimes misjudge the “best” supplier.

Tips:

Compare three quotations using the same drawing revision and tolerance notes. Request a landed-cost table, not only a piece price. Check whether inspection is included. Clarify who pays for rework. I would also test one small batch before signing a long-term agreement. It feels slower, but it exposes weak communication early. My own caution: delivery promises are often optimistic when capacity data is missing. Ask for evidence.

Buyer Selection Framework: RFQs, PPAP, DFM Reviews, and Risk Control

Top Machining Parts Suppliers for Global Buyers

Choosing a machining supplier requires more than comparing hourly rates. A strong RFQ should define alloy grade, drawing revision, tolerances, surface finish, annual volume, and inspection needs. During supplier evaluations, request sample inspection reports and confirm the available equipment. A five-axis mill may reduce setups, while in-process probing can prevent repeated errors. Ask how nonconforming parts are contained, documented, and corrected. Small gaps matter.

PPAP evidence can reveal process maturity before production begins. Review dimensional results, material certificates, capability studies, control plans, and approval records. A practical DFM review should happen before cutting metal. Engineers may identify thin walls, deep pockets, sharp internal corners, or unrealistic tolerance stacks. These details affect cycle time and scrap risk. Still, DFM advice is not always perfect. One suggested change may improve machining but weaken assembly performance. Keep the discussion open and record every approved revision.

Tips: Send one controlled drawing package. Use a clear part number and revision code. Ask for a milestone schedule with inspection points. Review first-article results before releasing full volume. For risk control, assess backup equipment, raw-material traceability, packaging methods, export documentation, and communication response time. A supplier that reports a problem early is often safer than one promising zero defects. Measure twice. Trust evidence.

Back To Top